As a cement testing instrument supplier, I’ve spent the last 12 years working hand-in-hand with cement plants, quality labs, and construction material testing facilities across 17 countries. Most days, I stand beside lab managers as they unbox a new automatic Blaine air permeability apparatus, or troubleshoot a vibrating table that won’t settle into the precise frequency it needs to. Over that time, I’ve learned that the most common mistake teams make isn’t in how they run tests—it’s in not understanding that the accuracy of every single cement lab result starts with the quality control of the instruments themselves. Cement testing isn’t just a box-ticking exercise for regulatory compliance; it’s the backbone of building highways that won’t crack, bridges that will stand for a century, and high-rise apartments that keep families safe. If your testing instrument is off by even a tiny margin, your cement strength results could be 5% too low, leading to over-ordering (and wasted millions in material) or 5% too high, risking catastrophic structural failure. That’s why today, I’m breaking down the quality control measures we at our company enforce for every single instrument we build, calibrate, and support—and why these steps aren’t just for our in-house process, but for every lab that uses our equipment. Cement Testing Instrument
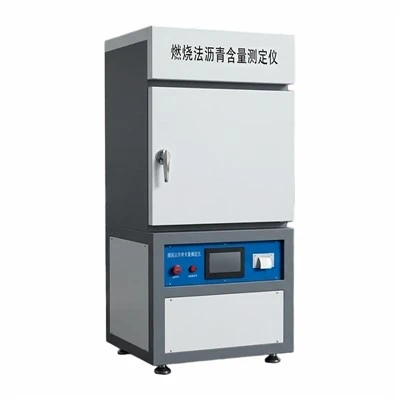
First, let’s start with incoming material inspection—because even the best design falls apart if you build it with bad parts. For example, our automatic compression testing machines rely on precision load cells to measure the force applied to cement cubes. We don’t just order load cells from any manufacturer; we have a dedicated team that runs 48-hour stress tests on every incoming load cell before it even touches an instrument frame. We test for linearity, hysteresis, and repeatability under both room temperature and the 10°C to 40°C range that labs operate in. A few years back, a batch of load cells from a new supplier came in 2.3% under their rated capacity. Instead of rushing to build machines and then having to scrap them, our inspection team caught that discrepancy on day three of testing. We sent the load cells back, and that supplier still doesn’t work with any cement testing lab we reference today. It’s a small step, but it’s the first line of defense against instrument error. For other critical components—like the vibrating tables used to compact cement mortar, or the water baths for setting time tests—we inspect every part for material consistency. We test the steel used for machine frames for tensile strength, ensuring it won’t warp after 10,000 cycles of loading a 50kN cement cube. We test the rubber pads under vibrating tables for compression set, so they don’t lose their ability to dampen unwanted vibration after months of use. No part leaves our warehouse without passing these checks.
Next is the in-process calibration during manufacturing, which is where we catch errors before an instrument is fully assembled. For any cement testing instrument, precision is everything—so every step of putting a machine together has a built-in calibration checkpoint. Take our Blaine air permeability apparatus, used to measure the fineness of cement, a key factor in how quickly it sets and its strength. During assembly, we first calibrate the manometer (the part that measures air flow) using a precision reference air flow meter traceable to national standards like NIST (National Institute of Standards and Technology) in the U.S. or PTB in Germany. We don’t wait until the entire apparatus is built to check this—if the manometer is off by even 0.1 kPa, the fineness result will be wrong. Another example: our automatic Vicat testers, which measure the initial and final setting time of cement. The needle on the Vicat tester has to drop exactly 10mm for initial set and 0.5mm for final set, per ASTM C194 standards. During assembly, we use a digital height gauge (accurate to 0.001mm) to test every needle’s drop distance before we mount it to the machine. We’ve had cases where a technician adjusted the needle mount slightly off-center during assembly, and the height gauge caught that before the machine was packaged. That would have meant a lab wasting time running tests with an instrument that gave false set time results. This step isn’t just about checking work—it’s about embedding precision into every part of the build.
Then there’s the post-assembly functional testing, which is the most rigorous step in our process. This is when we run the instrument through a full battery of tests using cement samples of known composition, so we can compare our instrument’s results to the certified values from national reference labs. For example, when we finish building a compression testing machine, we test it with 50mm cement cubes that have been certified by the National Ready Mixed Concrete Association (NRMCA) to have a 28-day compressive strength of 52.3 MPa. We run three separate compression tests on these cubes, and the machine’s average result has to be within ±0.5 MPa of that certified value—no exceptions. If it’s off, we take the machine apart to check the load cell, the alignment of the platens, or the calibration of the control system. A few years ago, we had a machine that gave a 52.9 MPa result on those certified cubes, just 0.6 MPa over the limit. We traced the problem to the platen alignment—one of the platens was tilted by 0.02 degrees, which might sound tiny, but it’s enough to skew the force measurement. We re-aligned the platens, re-tested, and got the correct 52.1 MPa result. That’s the kind of detail that makes our instruments reliable for labs. For other instruments, like automatic setting time testers, we use certified cement samples with documented initial set times of 120 minutes and final set times of 195 minutes. The machine has to record these times within ±2 minutes to pass functional testing. Anything outside that range gets sent back for adjustment.
But quality control doesn’t stop when the instrument leaves our factory. We also have a comprehensive calibration and verification program that every instrument undergoes before delivery, plus ongoing support for labs that use our equipment. We calibrate every instrument’s control system, sensors, and moving parts using traceable reference standards—meaning our calibration equipment is itself calibrated against national standards, creating an unbroken chain of accuracy that labs can trust for regulatory compliance. For example, all of our load cells are calibrated against NIST-traceable dead weight testers, so when a lab uses our compression machine for tests that have to meet ASTM or EN standards, they can prove the instrument’s accuracy to regulators. We also run a 72-hour continuous operation test on every instrument, to make sure it can handle long runs without drift. Our vibrating tables, for example, run 24 hours a day for three days straight, compacting mortar samples every hour. We check their frequency every 12 hours, and it has to stay within ±1 Hz of the 50 Hz (or 60 Hz, depending on the market) required for mortar compaction. This catches issues like loose motor mounts or worn belts that would cause frequency drift over time.
Another key part of our quality control is validation against global standards, because cement testing requirements are strict worldwide. We don’t just build instruments that work for our internal tests—we design them to meet or exceed ASTM, EN, and IS (Indian Standards) specifications, because those are the benchmarks that labs use. For example, our air permeability apparatus meets the exact dimensions outlined in ASTM C204, from the size of the test sample to the flow rate of air through the apparatus. We also test each instrument for consistency across all units we build. If we make 10 Blaine apparatus in a month, all 10 have to give the same result when tested with the same certified cement sample. We’ve had a batch of 5 apparatus that had a 1.2% difference in fineness results when tested with the same cement, and we realized the filter paper used in the test had slightly different porosity from a new supplier. We switched back to our original filter paper supplier, and all 5 units passed the consistency check. That’s the kind of attention to detail that ensures every lab gets the same reliable results, no matter which instrument they buy from us.
Now, I know that some of you might be wondering: why does all this matter? For a small lab in a rural area, or a large plant testing hundreds of samples a day, the accuracy of your cement testing instrument isn’t just a technical detail. It’s about building something that lasts. A few years back, we worked with a small cement plant in Brazil that was using a 5-year-old testing instrument from a generic supplier. Their strength results were consistently 4% lower than the certified values, so they were adding 5% more clinker to each batch to meet strength requirements. That extra clinker was costing them over $200,000 a year in raw material costs, not to mention increasing their carbon footprint. When they switched to one of our calibrated compression machines, their results were accurate within 0.3% of certified values. They reduced their clinker usage by 5% and cut their annual costs by nearly $210,000. That’s the real impact of good quality control in cement testing instruments.
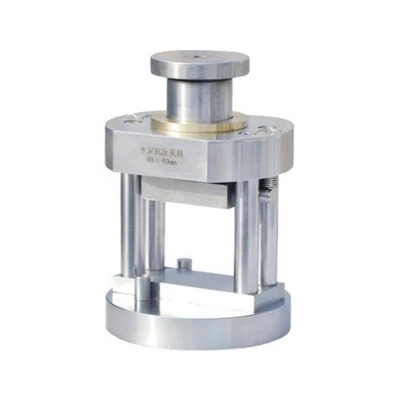
At our company, we don’t just sell instruments—we sell peace of mind. Every quality control step I’ve outlined here is part of our promise: that when you receive a cement testing instrument from us, it’s been built, tested, and validated to give you accurate, consistent results every time. We also offer on-site calibration services for every instrument we sell, so if a lab needs to re-calibrate their machine mid-cycle, our technicians can be there in 48 hours (for most locations) to do it without disrupting their workflow. We also provide a 3-year warranty on all parts and labor, because we stand behind our quality control process.
Cement Testing Instrument If you’re in the market for a new cement testing instrument, or if your current instruments are giving inconsistent results that are costing you time and money, we’re here to help. Our team of engineers has over 100 years of combined experience in cement testing, and we can help you find the right instrument for your lab’s needs, whether you’re a small testing lab, a large cement plant, or a construction materials company. We’ll walk you through every part of the quality control process so you know exactly what you’re getting when you work with us. Don’t let inaccurate testing results put your projects, your budget, or your reputation at risk. Reach out to our team to start a conversation about your cement testing needs today.
References
- American Society for Testing and Materials. (2022). Standard Test Method for Fineness of Hydraulic Cement by Air Permeability Apparatus (ASTM C204). ASTM International.
- European Committee for Standardization. (2021). Cement – Test methods – Determination of setting time and soundness (EN 196-3). CEN.
- National Institute of Standards and Technology. (2020). Traceable Calibration Services for Force and Pressure Measurement. NIST Special Publication 250.
Hebei Wanluda Testing Instrument Equipment Co., Ltd.
As one of the most professional cement testing instrument manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy advanced cement testing instrument made in China here from our factory.
Address: Zhouguantun Village, Xian County, Cangzhou City, Hebei Province, P.R.China
E-mail: wldinstrument@163.com
WebSite: https://www.wldinstrument.com/
